Minimum Flange Length in Sheet Metal Bending
Time : Sep 18, 2026 View : 0
Introduction: Why Flange Length Matters in Press Brake Design
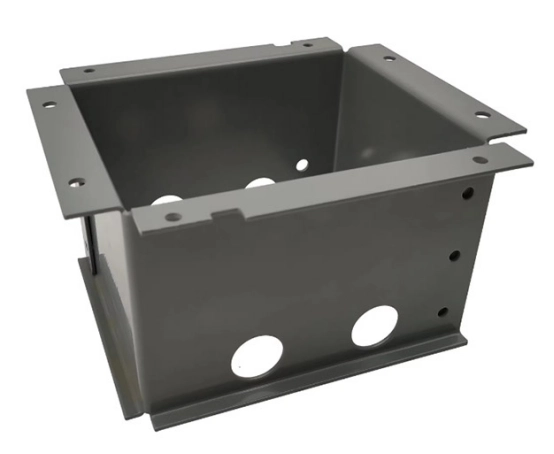
A short flange can turn a straightforward press brake job into a scrap problem. The sheet may not sit securely on the die shoulders. The punch can strike an edge. The bend angle may drift along the part.
Minimum flange length is the shortest distance from the bend line to the sheet edge that can be formed reliably with a selected punch and die. It is not fixed. Sheet thickness, inside radius, material strength, V-die opening, and the bend method all affect it. A sound design leaves enough process support, not just enough metal to look right in CAD.
What Is Minimum Flange Length in Sheet Metal Bending?
Flange length is measured from the bend tangent or bend line to the outside edge of the formed leg. The measurement convention should match the drawing standard. That matters with tight tolerances.
Minimum flange length is different from bend allowance and bend deduction. Those values create a flat pattern. They do not confirm that the flange can sit on a press brake die without slipping or colliding with tooling. A flange can be correct in a flat layout and still be too short to form consistently.
Why Minimum Flange Length Is Critical for Press Brake Parts
During air bending, the workpiece rests on two die shoulders while the punch drives the bend. A very short leg has little bearing area. It can tilt, roll into the die opening, or pull a nearby feature out of position.
The symptoms are familiar on the shop floor: variable angles, edge marks, a bow near the corner, or a flange out of square. Stainless steel can add springback and force. A welded assembly can magnify a small error because the mating panel no longer lines up. A few extra millimeters may avoid a new setup, special tooling, or rework.
How to Calculate the Minimum Flange Length
The calculation starts with the tool, not a favorite rule of thumb.
Start with the V-die opening
For a preliminary air-bending estimate, many fabricators use:
Minimum flange length ≈ 0.7 × V-die opening
With a 16 mm V-die, that gives about 11.2 mm. Treat it as a screening value. The production minimum may be larger because the flange must clear the punch nose and stay stable through the stroke. Tool data should take priority.
Consider sheet thickness and bend radius
Thicker material normally requires a larger V-die opening, which increases the flange envelope. The inside bend radius matters too, especially on thick plate.
For mild steel, an inside radius close to material thickness is a useful air-bending starting point. It is not a promise. High-strength grades, stainless steel, and aluminum can behave differently at the same thickness. Grain direction and temper change the result.
Add a manufacturing safety margin
Use more than the calculated minimum for offset bends, hems, narrow returns, or holes close to the bend. Tight tolerances deserve margin. A flange that works during setup may not be robust across a long batch.
How Tooling and Bending Methods Change the Recommendation
Air bending is flexible and common, but the flange depends heavily on V opening and shoulder contact. Bottoming brings the sheet farther into the die and can improve repeatability. It also demands more force. Coining can hold a precise angle, yet its high tonnage makes it specialized.
A narrow V-die may help a short flange in one setup. It also raises force and can mark soft aluminum. A wide V-die lowers force but often needs a longer flange and produces a larger radius. Punch nose, die shoulder, tooling height, and machine capacity should be checked as one system.
Material and Thickness Effects on Minimum Flange Length
Mild steel usually tolerates standard air-bending practice. Stainless steel brings more springback and may need a larger allowance for force and angle correction. Aluminum is relatively soft, so a narrow die or damaged shoulder can leave visible marks. Brass and other soft alloys may distort at the edge when support is marginal.
Surface protection can influence the choice. A cosmetic stainless panel may need film and a less aggressive tool condition. A hidden bracket has a different priority. The correct minimum is tied to material grade and the part’s job.
Sheet Metal DFM Checklist Before Releasing the Drawing
Confirm these points before releasing the part:
-
Sheet thickness and material grade are stated.
-
Inside bend radius matches the intended tooling.
-
V-die opening and punch geometry are available for review.
-
Every flange meets the practical minimum, not just the CAD minimum.
-
Holes and slots have enough distance from the bend line.
-
Bend relief is included at corners and near cutouts.
-
Grain direction is noted when cracking or appearance matters.
-
Bend sequence has been checked for tool interference.
-
Flat pattern and bend deduction are based on the chosen process.
-
Functional tolerances are separated from cosmetic tolerances.
-
Welding or coating after bending is considered.
A useful drawing note is: “Minimum flange dimensions to be confirmed by the manufacturer during DFM review.” It leaves room for a practical tooling decision.
Common Minimum Flange Design Mistakes
The “2t” rule is often repeated as if it applies to every job. It does not. Another mistake is checking the flange against material thickness while ignoring the V-die opening. Holes are placed close to a bend because the flat pattern looks clean. Relief is omitted. Narrow tooling is selected without checking tonnage.
Laser cutting accuracy does not remove bending variation. Springback and bend sequence still matter. A drawing without a tool-access review can pass inspection on paper and fail during forming.
FAQ: Minimum Flange Length in Press Brake Bending
Q: What is the common minimum flange length for air bending?
A preliminary estimate is around 0.7 times the V-die opening. Confirm it against the punch, die shoulders, material, and tolerance.
Q: Can a press brake bend a flange shorter than the standard recommendation?
Sometimes. Special tooling, a different sequence, or a small design change may make it possible. Prove it with a sample rather than assume it from a formula.
Q: What should engineers send for a flange-length review?
Send the 2D drawing or 3D model with material, thickness, quantity, tolerances, finish, and critical assembly dimensions. A photo of the installation can reveal clearance issues.
How Deshibo Machinery Supports Production-Ready Sheet Metal Designs
Deshibo Machinery connects engineering review with fabrication. Its in-house CAD and mechanical engineering support can check a drawing before cutting starts. The production route can combine metal laser cutting and bending with welding or CNC machining when a formed part needs accurate holes, threads, or mating surfaces.
The company works with stainless steel, mild steel, aluminum, and brass. Its custom sheet metal welding service can continue the job after bending. Drawings, sketches, and 3D files support prototypes, small batches, and OEM production.
Conclusion
Minimum flange length is a tooling decision expressed in the drawing. Check the V-die opening, material, thickness, bend radius, and machine capacity together. When the limit is unclear, contact Deshibo Machinery and send the model and requirements. A short DFM review can prevent a long production problem.
