Bend Allowance vs Bend Deduction: Sheet Metal Guide
Time : Sep 23, 2026 View : 0
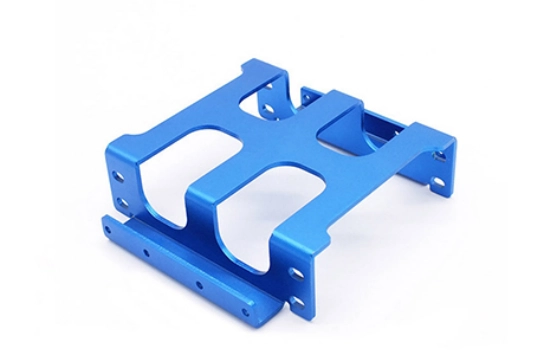
A sheet metal part can leave the press brake with the right angle and still miss its target dimensions. Metal stretches outside a bend and compresses inside it. The neutral layer between them keeps nearly the same length. Bend allowance and bend deduction describe that change from different directions.
What Is Bend Allowance?
Bend allowance is the length of the neutral layer that follows the bend arc. It is the extra length needed in the flat blank to produce the finished part. CAD sheet metal tools use it to unfold a model before laser cutting.
Definition of Bend Allowance
The neutral layer position depends on material, thickness, radius, tooling, and forming method. A default value can work on one job and fail on the next.
Bend Allowance Formula
The common formula is:
BA = π × A / 180 × (R + K × T)
BA is bend allowance. A is the bend angle in degrees. R is the inside bend radius. T is material thickness. K is the K-factor, the neutral layer position expressed as a fraction of thickness.
A 90 degree bend in 2 mm mild steel with a 2 mm radius and K-factor 0.33 gives about 3.14 mm. Use a measured production bend table.
Factors That Affect Bend Allowance
Material grade, die opening, punch radius, and grain direction all affect the result.
Record these details in the process plan.
What Is Bend Deduction?
Bend deduction starts with the finished outside dimensions. It tells the engineer how much to subtract from the sum of the flange lengths to obtain the flat length.
Definition of Bend Deduction
For an L bracket, add the two outside flange dimensions, then subtract the bend deduction to find the laser cut length.
Bend Deduction Formula
The basic relationship is:
BD = 2 × OSSB − BA
BD is bend deduction. OSSB is outside setback. BA is bend allowance. For a typical 90 degree bend, outside setback is often calculated as:
OSSB = R + T
The flat length then becomes:
Flat Length = Flange 1 + Flange 2 − BD
Using the example above, OSSB is 4 mm. Bend deduction is 2 × 4 − 3.14, or 4.86 mm. If the outside flanges are 40 mm and 60 mm, the blank length is 95.14 mm.
Why Bend Deduction Is Useful
Bend deduction is practical when inspection uses outside dimensions and provides a quick drawing to cutting file check.
Bend Allowance vs Bend Deduction: Key Differences
The two terms are linked. They are not competing manufacturing systems. Bend allowance describes the length along the neutral layer. Bend deduction describes the amount removed from outside dimensions. Both can lead to the same flat pattern when the inputs are consistent.
| Item | Bend Allowance | Bend Deduction |
| Calculation focus | Neutral layer arc length | Amount removed from outside dimensions |
| Typical use | CAD flat patterns | Drawing and blank size checks |
| Main inputs | K-factor, radius, thickness, angle | OSSB and bend allowance |
| Best fit | Complex parts and multiple bends | Parts dimensioned from the outside |
Check which convention the CAD system or machine program expects.
Worked Example: Calculating a 90 Degree Sheet Metal Bend
Consider a mild steel bracket. The sheet is 2 mm thick. The inside radius is 2 mm. The bend angle is 90 degrees and the working K-factor is 0.33.
The bend allowance is:
BA = 3.1416 × 90 / 180 × (2 + 0.33 × 2) ≈ 3.14 mm
Outside setback is:
OSSB = 2 + 2 = 4 mm
So the bend deduction is:
BD = 2 × 4 − 3.14 = 4.86 mm
With outside flange dimensions of 40 mm and 60 mm:
Flat Length = 40 + 60 − 4.86 = 95.14 mm
Treat the result as a starting point. Tool wear and material batches can move it slightly.
How to Choose the Right Calculation Method
Choose the method that matches the drawing and inspection method.
Use Bend Allowance When
-
A CAD model creates the flat pattern.
-
The design uses several bends or a closed box.
-
The neutral layer position must be controlled across materials.
-
A validated database of K-factors is available.
Use Bend Deduction When
-
The drawing calls out outside flange dimensions.
-
A quick blank size calculation is needed.
-
Inspection is performed from outside faces.
-
Existing press brake tables are organized by bend deduction.
Best Practice
Keep a bend table for each material and thickness. Record tooling and measured flange lengths. Run a prototype before releasing a batch. On an enclosure job, this exposed a 1 mm flange error before production.
Common Sheet Metal Bending Errors and How to Prevent Them
Error 1: Using the Wrong K-Factor
A K-factor from another alloy or tooling setup shifts every bend. Calibrate supplier data with a test bend.
Error 2: Ignoring Springback
Springback opens the angle after release. Stainless and high strength steel need attention. CNC compensation and planned overbend improve control.
Error 3: Confusing Inside and Outside Dimensions
Mark the dimension reference on the drawing. A 40 mm inside flange is not a 40 mm outside flange. This single clarification prevents many shop floor questions.
Error 4: Forgetting Tooling and Bend Sequence
A correct calculation cannot fix tool interference. Review bend sequence and collision points before cutting.
How Deshibo Machinery Ensures Accurate Sheet Metal Bends
Yantai Deshibo Precision Machinery Co., Ltd. has provided product development, prototypes, and volume production since 2018. Its workflow links metal laser cutting and bending with custom sheet metal welding parts.
The engineering review starts with a 2D drawing or 3D CAD file. Material, thickness, radius, tolerances, and finish are checked before releasing the flat pattern. For assemblies that combine turned or milled features, CNC machining can be included in the same supply plan.
Conclusion: Get Accurate Sheet Metal Parts from the Start
Bend allowance follows the neutral layer. Bend deduction subtracts the bend effect from outside dimensions. Use the term that matches the drawing and software, then verify the result with a real test bend.
Have a sheet metal part to manufacture? Send a 2D drawing or 3D CAD file to Deshibo Machinery for a quotation covering laser cutting, bending, welding, or complete custom fabrication.
FAQ
Q: Is bend allowance the same as bend deduction?
No. Bend allowance is the neutral layer arc length. Bend deduction is the value subtracted from outside flange dimensions. They are mathematically related.
Q: What K-factor should be used for stainless steel?
There is no universal value. Start with a value from the material and tooling supplier, then confirm it with a measured test bend.
Q: Which method is better for CNC press brake work?
Either method can work. The important point is consistency between the CAD flat pattern, bend table, machine program, and inspection dimensions.
Q: Can bend calculations prevent all dimensional variation?
No. They reduce predictable error. Springback, material batches, tooling wear, and operator setup still require process checks.
